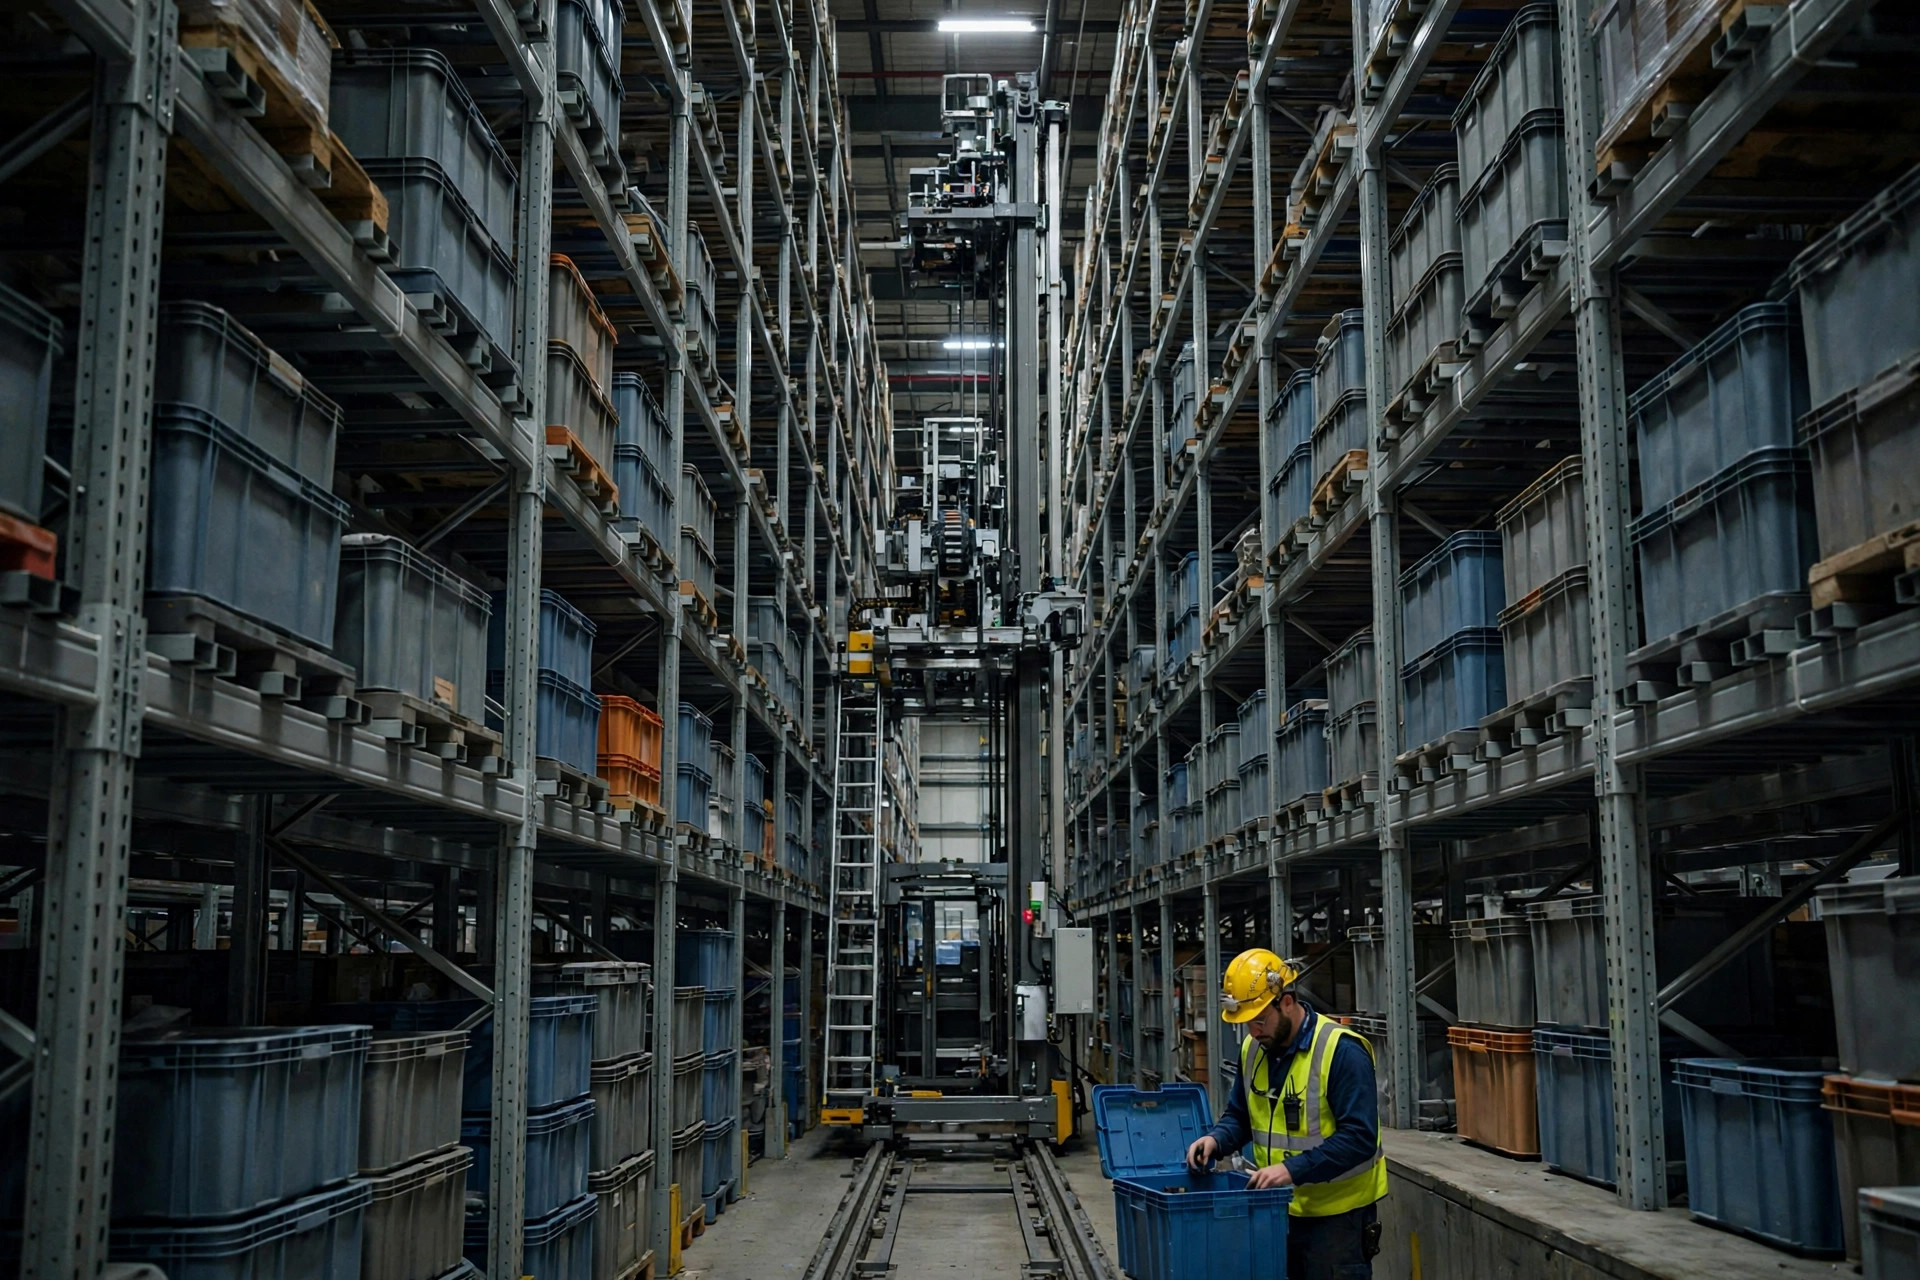
Stacker crane preventive maintenance is a lesson most people learn at 2 a.m., by phone. A third-party warehouse in the Midwest had a crane stop dead in the middle of a high-bay aisle, fork halfway out, a pallet wedged at the mouth of a location. About 400 outbound orders were already backing up, and nobody on the night shift dared to touch the machine. The manufacturer's engineer arrived after dawn. The fix took roughly 40 minutes. The culprit was a loose encoder connector, not a burned motor, not a broken structure. The cable cost next to nothing; the lost night cost a hundred times more. Cranes rarely fail with a bang. They fail like a bad tooth: a little looseness here, a little dirt there, then everything hurts at once on the worst shift.
What a crane is actually afraid of
Think of a stacker crane as a forklift on rails in a very narrow hallway that has to know exactly where it is at all times — a train with a fork. Horizontal speeds around 180 meters per minute and lift speeds around 60 sound impressive, but speed is not the hard part. Knowing its position and stopping within a few millimeters is. The encoder reports position, the rails carry the load, and the safety circuits stand behind all of it. If any one of those three gets vague, the control system does the only responsible thing and stops: it refuses to guess. A crane unsure of its position that extends its fork anyway could drive a pallet into the wrong location or into the rack itself.
Most warehouses price a crane by purchase cost and rated pallets per hour. I price it by unplanned downtime. Run the rough math: a crane scheduled for about 6,000 hours a year loses about 60 hours of capacity for every point of availability it gives up. At roughly 60 pallets an hour, that is about 3,600 pallets that simply never happened. See downtime as lost capacity rather than a maintenance bill, and the conversation flips: inspection is not overhead, it is how you buy capacity back.
Stacker crane preventive maintenance, system by system: rails, encoders, and safety circuits
Keep three separate ledgers. One blended checklist saying "crane checked" tells you nothing when something breaks on a Tuesday night.
Rails come first, and joints matter more than straight sections. A joint step under 1 millimeter can wear past 2 millimeters, and every wheel crossing makes the crane shudder. One shudder is nothing; tens of thousands chew through wheels, bearings, and motor current. The method is unglamorous and it works: check joints monthly with feeler gauges and a level, listen to the travel sound, and watch the motor current curve for a repeating spike. A current curve is like a heart monitor: flat is healthy, and a spike repeating at the same travel position points at a rail problem there. Tolerances should follow the manufacturer's manual, not a blog post.
Encoders are the second system, and here is the part that surprises people: eight times out of ten, the encoder itself is fine and the cable is the problem. Vibration, oil, and a bend radius tighter than the cable likes will make the signal drop out for a fraction of a second, just long enough for the controller to lose trust in its position. A food distribution center I worked with chased a recurring position error for weeks, replaced the encoder, and watched the error stay. The real fault was a signal wire chafed inside a cable chain, breaking contact only when the chain bent to one particular angle. A new cable and better chain routing fixed it for less than a tenth of the encoder replacement. My rule is simple: check the cable, the connector, and the shield grounding first, and swap the encoder only after those three check out. Cables are far more fragile than the device they serve.
Safety circuits are the backstop, and they are the one place where cutting corners is indefensible. Emergency stops, safety gate switches, overspeed protection, fork anti-drop devices, and aisle-end limits are wired in series, and any one opening must stop the machine cleanly and immediately. Inspection means actually tripping them, not glancing at a green light. Test the emergency stop and safety gates at least once a month, and record stopping time and distance. Some managers call that wasted capacity. I call the alternative worse: a safety circuit never genuinely tested is a rumor, not a safeguard. After an incident, those records are asked for first.
| Inspection item | Suggested interval | What to check | What happens if you skip it |
|---|---|---|---|
| Floor and top rail joints, straightness | Monthly | Joint steps, wear, unusual noise | Vibration eats wheels and bearings |
| Encoder cables and connectors | Monthly | Chafing, looseness, shield grounding | Position loss, unexplained lockouts |
| Safety circuit live tests | Monthly | E-stop, gates, limits actually tripped | Protection fails when it matters most |
| Travel and guide wheels | Quarterly | Wear, cracks, clearance | Drift gets worse and damages rails |
| Fork chains and ropes | Quarterly | Stretch, lubrication, broken wires | Fork drop risk, pallet damage |
| Motor current curve review | Quarterly | Repeating spikes, abnormal load | Small faults grow into multi-day repairs |
The line between money well spent and theater
Now the blunt part. Some warehouses buy a full online monitoring package, vibration sensors everywhere, and a predictive dashboard, while their basic inspection sheet sits empty. That is theater: racing gauges on a car whose oil has never been changed. Until monthly hands-on inspection, quarterly deep checks, and a complete fault log are actually happening, any fancy monitoring is a pseudo-need. Do the boring work first, then decide what sensors add.
Three things are worth paying for. Spares first: one encoder, one set of travel wheels, and the common connectors and cables, kept on site, models matched to the manufacturer's manual, long-lead items ordered at least two months ahead. Training second: night-shift operators who can read an alarm code and run a first-pass check are worth more than any hotline. A fixed window third: about two hours a week, protected even when orders pile up. A plan with no protected window is a wish, not a plan.
Staffing has three honest answers. In-house suits a warehouse with at least two dedicated technicians: fast response, but you carry training and spares costs. A service contract suits a smaller fleet, with response time and spares responsibility written into the contract and per-visit versus annual pricing compared on real numbers, not vibes. Doing nothing is not saving money: it converts small repairs into major overhauls and planned stops into midnight emergencies. Most mid-size warehouses go hybrid: daily checks in-house, quarterly and annual work contracted out.
Stacker crane preventive maintenance: three traps I keep seeing
Trap one is lubrication by feel. Too much grease and dust sticks to the rail and turns into grinding paste; too little and wheels run dry. Lubricant type, quantity, and interval belong to the manufacturer's manual, full stop. Put a lubrication map on the wall, and log who greased what, how much, and when. Trap two is repairing without recording. Part replaced, reason, last occurrence, time taken: five columns kept for a year give the machine a medical history. Without it, you fix the same fault in the same place twice. Trap three is treating alarms as noise. The same position-deviation alarm three times in a month is not bad luck; it is the system warning you early. My rule is three strikes and you hunt the root cause, no resetting and moving on until you find it.
Here is the counterintuitive part, and I will say it plainly because it annoys people: more maintenance is not always better. Unplanned teardowns and constant recalibration introduce fresh looseness and fresh error. The value is in rhythm and records, not frequency: check what needs checking, leave alone what does not. A related judgment: slowing an old crane down can raise its output. Dropping horizontal speed from about 180 meters per minute to about 150 on a five- or six-year-old machine often calms vibration and current draw enough that availability climbs. Slower, but it stops less. Managers resist that math until they price a night of downtime.
So whether this money was worth it comes down to one number: did unplanned downtime hours go down over the year. A full sheet means nothing if that number stays flat; a plain routine means everything if it falls. That is the whole ledger for stacker crane preventive maintenance: fewer surprises, and when the crane stops, a clear reason you already saw coming.
By Da Liu, Automation Engineer